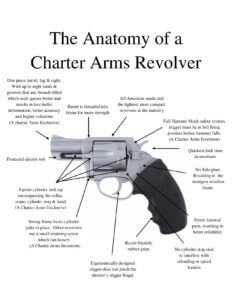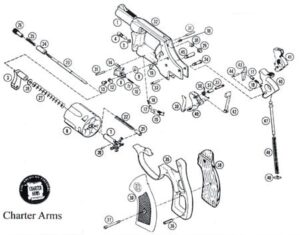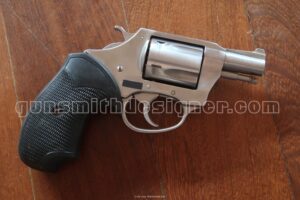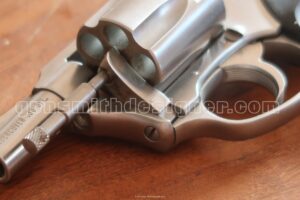
In this article, we will examine the design trade-offs chosen by the creators of the Charter Arms brand to produce their “Undercover” model. This is a small concealed-carry revolver chambered in .38 Special (a classic standard). I will focus specifically on the simplification of its mechanism, the grip frame/trigger guard assembly, and the main frame. Before diving into the Undercover itself, we will take a brief look back at the historical evolution of revolver frames.
A Brief Look Back
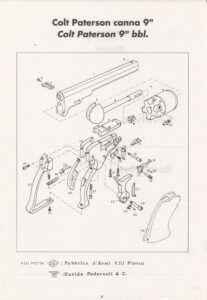
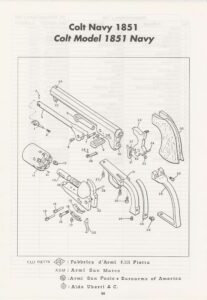
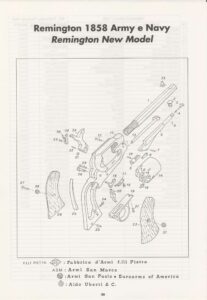
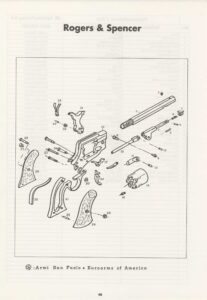
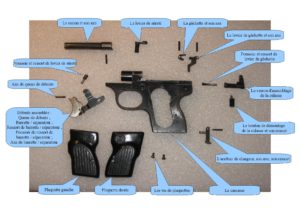
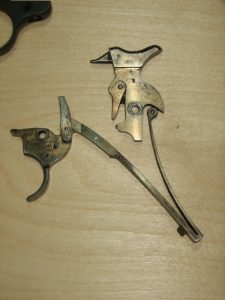
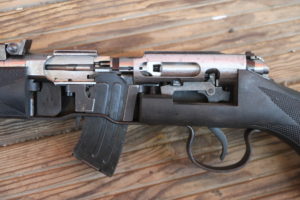
When looking back at the origins of revolvers—for instance, by studying the exploded views below—one can observe that design choices have evolved across different eras, depending on the manufacturing methods and resources available at the time.
The two key points of divergence lie in the frame and the barrel design. The cylinders, trigger mechanisms, and firing mechanisms have remained virtually unchanged, sharing highly similar designs during any given period.
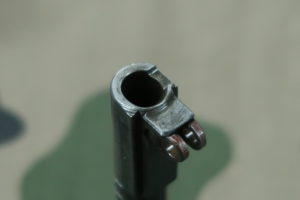
Octagonal and later cylindrical threaded barrels eventually superseded barrels featuring a lower web or lug extension. On open-frame firearms, this lower extension served to hold the cylinder in place and connect the barrel to the frame. The adoption of barrels threaded directly into the frame represents a significant simplification.
Frames were either manufactured as a single piece (such as the Remington 1858) or assembled from several smaller components (as seen on the Colt Paterson, Colt Navy 1851, Rogers & Spencer, and others). Splitting the main component into two or more parts reduces the risk of scrapping a complex piece that has already undergone extensive machining. It also creates openings that allow access to internal areas that would otherwise require specialized tooling to reach. This made it more cost-effective to mass-produce revolvers of equivalent quality using simpler manufacturing equipment. Open-frame firearms, offering less structural strength, were ultimately abandoned. As shown below, Charter Arms utilizes entirely different manufacturing levers to optimize production.
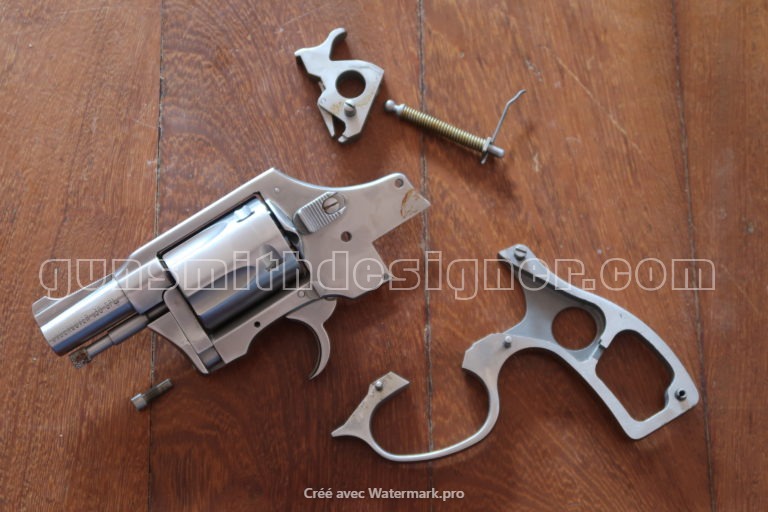
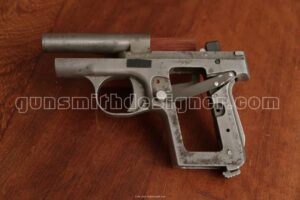
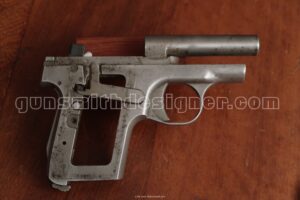
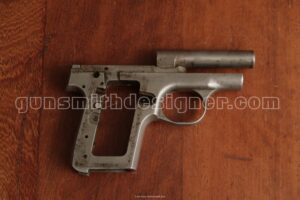
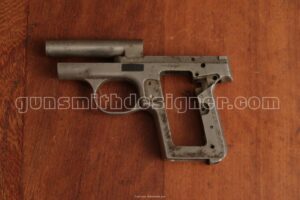
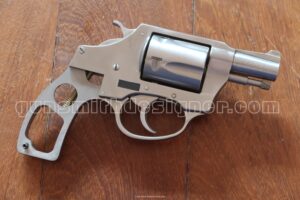
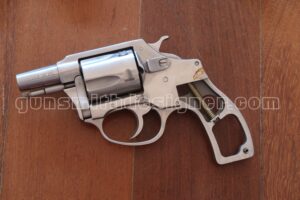
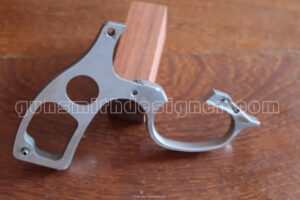
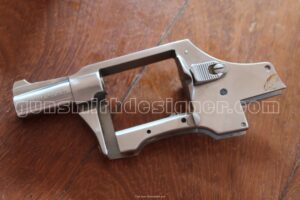
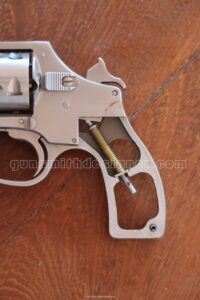
The most interesting feature of this firearm—and the one that prompted this article—is its grip frame assembly. This design choice effectively splits the revolver’s frame into two separate sections, completely eliminating the need for a traditional removable side plate. In terms of frame architecture, the Rogers & Spencer revolver (1863–1865) is quite close to our Charter Arms revolver. However, the Charter Arms mechanism was designed in 1964, roughly 100 years after the Rogers & Spencer.
Over time, new features were added to early revolvers: double-action capability, hammer safeties, swing-out cylinders, modern cartridge extraction, micrometric adjustable sights, ergonomic grips, barrel ports, and optical mounting rails. Regardless of the modern features added, it is clear that core structural optimization remains highly relevant today.
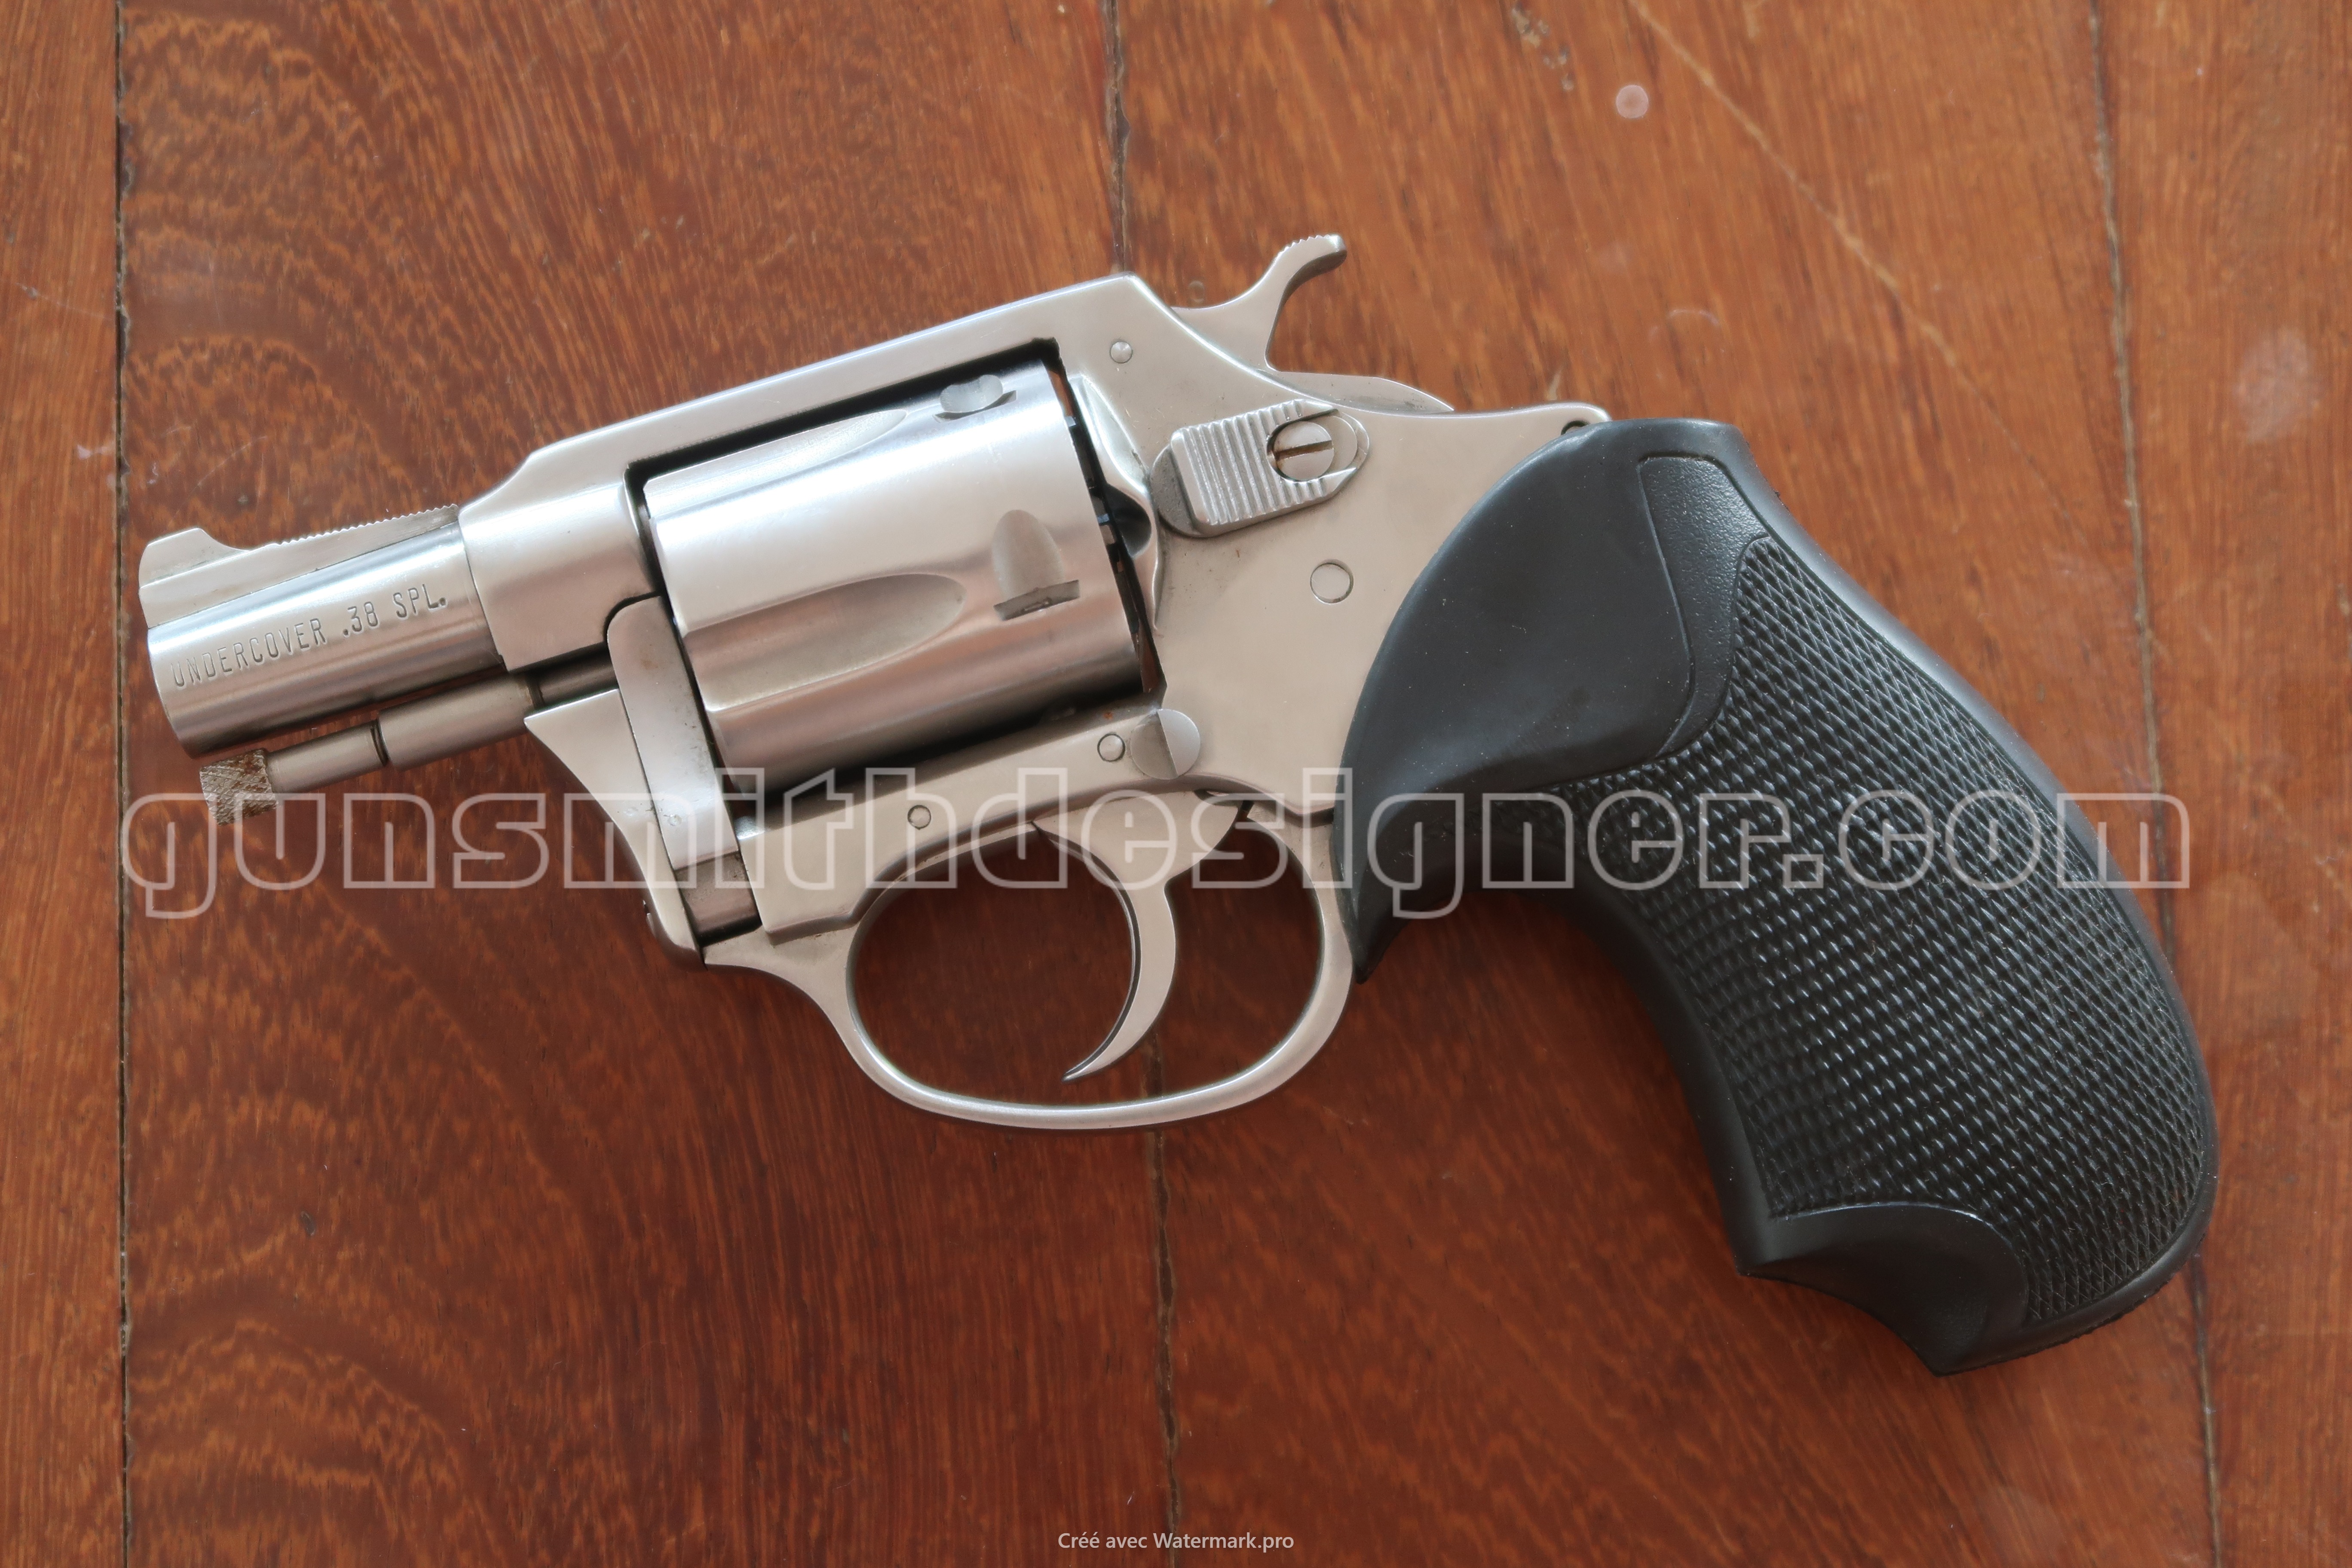
The Charter Arms Undercover Revolver in .38 Special
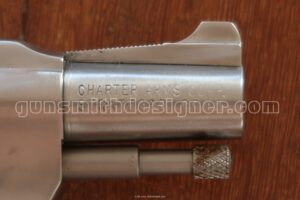
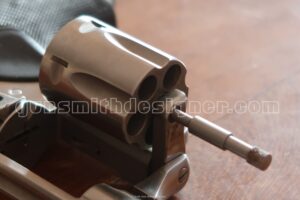
According to information obtained from the company, the barrel profile has evolved over the years. The specific model analyzed here pre-dates 1985. Newer barrel profiles include a shroud to protect the ejector rod, meaning this particular firearm is over 32 years old. I will let you judge its state of preservation for yourself.
A company presentation video is available here.
For gunsmithing and firearm tech enthusiasts, this video provides a look into the manufacturing environment of Charter Arms revolvers. Several videos are available on the company’s Facebook page: https://www.facebook.com/CharterFirearms/
Charter Arms employs 42 people.
Several components of the Undercover are produced using investment casting (micro-fusion). This is the primary lever Charter Arms uses to lower production costs and reduce manufacturing times. This is hardly surprising when you learn that the company’s founder (in 1964), Mr. Douglas McClenahan, was a former Ruger employee—a company known for its massive reliance on investment casting.
The Undercover was the brand’s very first model. It consists of 48 parts, and nearly 1.5 million units have been manufactured to date. This core platform serves as the foundation for various other models differentiated by caliber, barrel length, and finish.
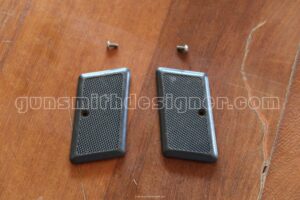
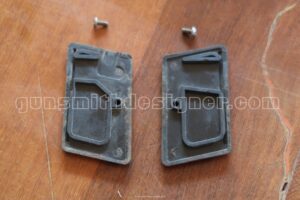
Thanks to its rubber grips, the firearm sits very naturally in the hand—at least in mine, as ergonomics depend heavily on individual hand morphology. I find it well-balanced.
Specifications :
-
- Weight: 590 grams (empty cylinder) ;
- Overall Length: 197 millimeters ;
- Width (Cylinder): 33 millimeters ;
- Width (Rubber Grips): 29 millimeters ;
- Barrel Length: 47.7 millimeters ;
- Rifling: 8 grooves, left-hand twist ;
- Single-Action Trigger Pull: 2.8 kg / 3 kg ;
- Double-Action Trigger Pull: 4.3 kg / 4.5 kg .
The Grip Frame / Trigger Guard Assembly
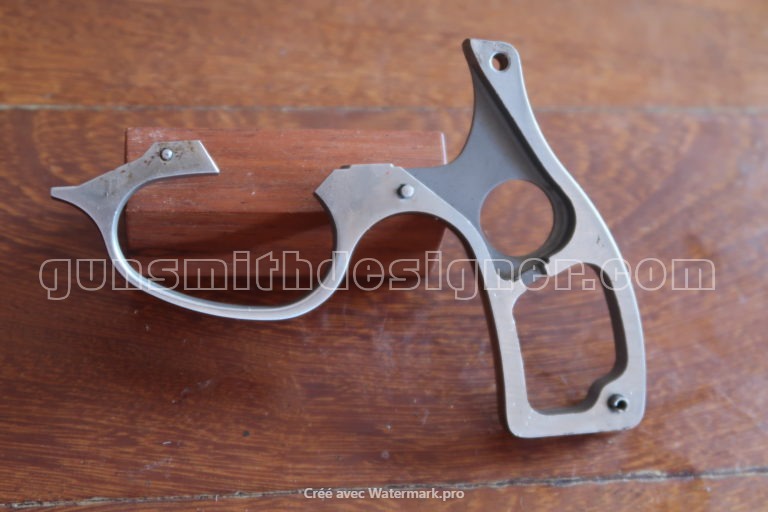
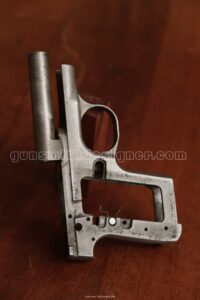
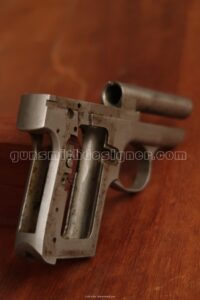
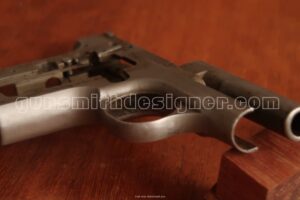
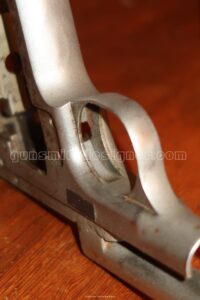
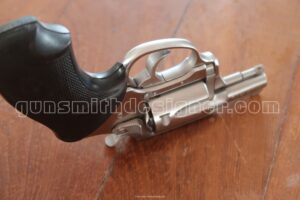
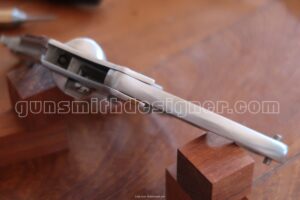
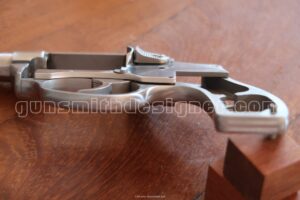
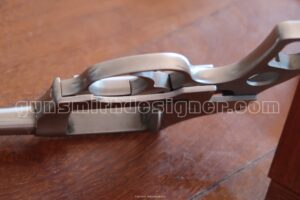
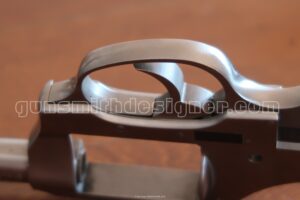
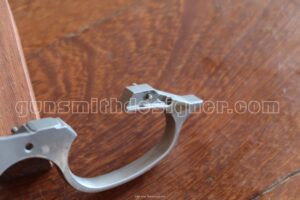
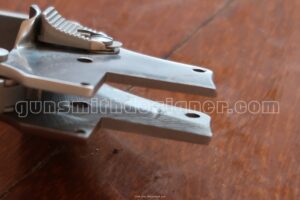
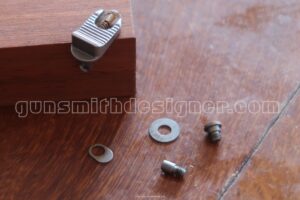
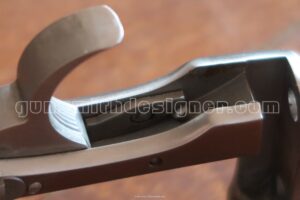
The grip frame and trigger guard are integrated into a single component. It is secured to the main frame at three points: one screw (3.5 mm) and two pins (2.5 mm and 2 mm) hold it in place. The part features a uniform thickness of 8 mm, making it robust yet lightweight.
The surface finish of the investment casting is exceptionally fine. Following the drilling of the pin holes, polishing appears to be the only step required after casting. The factory polish is very clean and smooth.
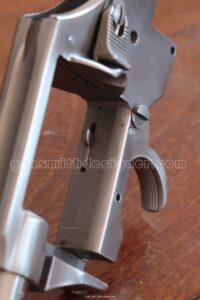
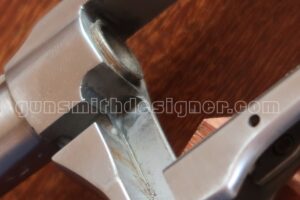
However, the fit between the main frame and the grip frame is not particularly seamless on this specific specimen. The gap between the two components is quite pronounced in several places, as seen in the photos. It would be interesting to see if this tolerance has been tightened and the play reduced on more recent production versions.
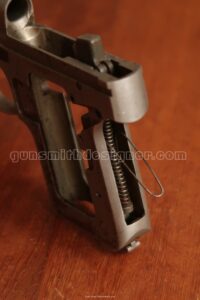
The grip frame also serves as the anchor point for the mainspring. It features a “round butt” profile. Because this component does not require extreme dimensional precision, utilizing investment casting for its production is a highly logical choice.
The Frame
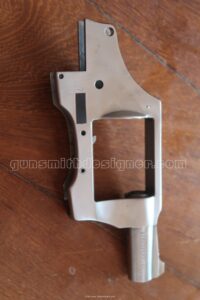
The main frame is also machined from an investment-cast blank.
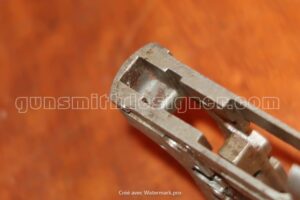
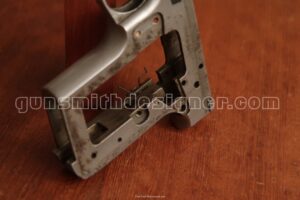
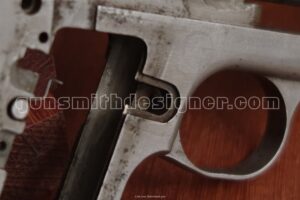
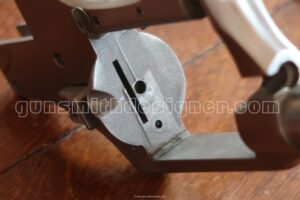
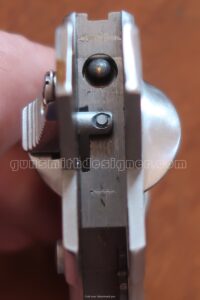
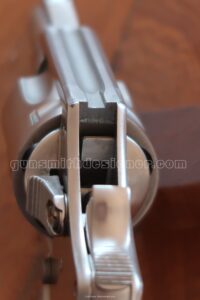
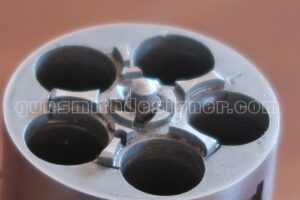
Looking at the recoil shield, you can see the slight “orange peel” texture left by the investment casting process. Only the critical functional surfaces have been polished—specifically, the areas where the cartridge rims and the cylinder star rest. This surface is easier to polish because it is slightly raised.
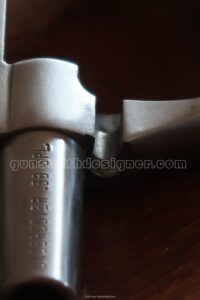
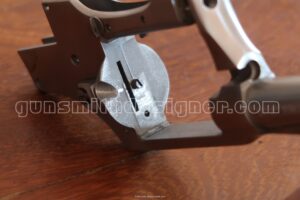
There is a right-angled notch machined into the frame, which I believe serves as a datum or reference point for positioning the component in fixtures before machining.
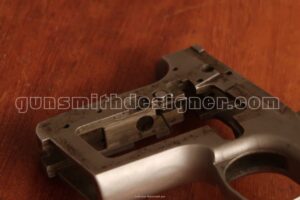
The interior is highly streamlined with no unnecessary machining operations. It is a far cry from the complex internal cuts of a Colt or a Smith & Wesson, yet it performs the exact same functions. The internal machined surfaces are clean; the manufacturer did not leave these areas raw from the casting process, and the cuts are well-executed.
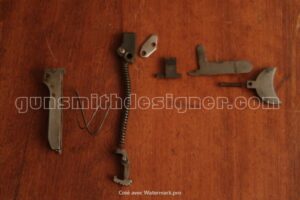
The cylindrical firing pin is frame-mounted and retained in its housing by a cross-pin. For ignition to occur, the transfer bar safety must be in its raised position, which only happens when the shooter fully depresses the trigger.
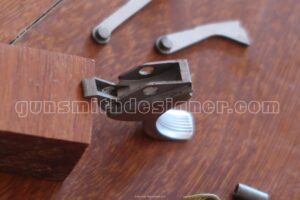
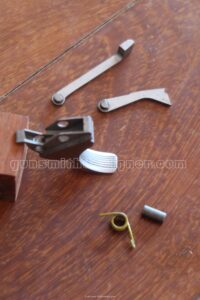
The cylinder release latch is minimalist. The thumb piece is another investment-cast part.
Unlike Colt or Smith & Wesson frames, which feature a removable side plate to access the internal mechanism, the Charter Arms frame is solid. The brand uses this as a marketing argument, claiming that a solid-frame design is inherently stronger.
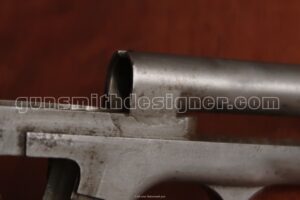
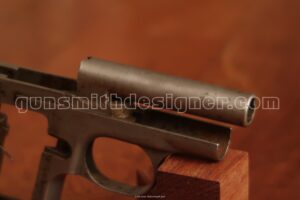
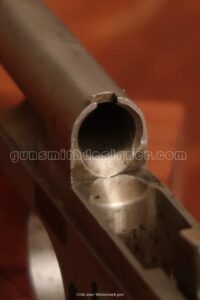
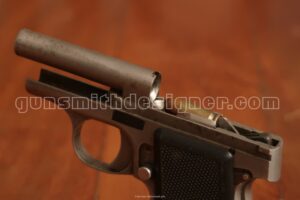
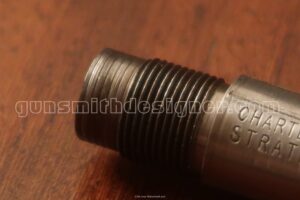
The barrel is threaded directly into the frame.
The Mechanism
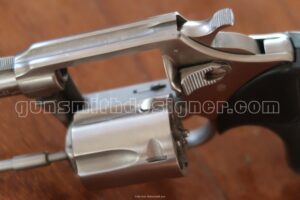
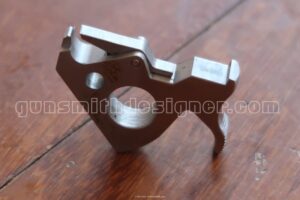
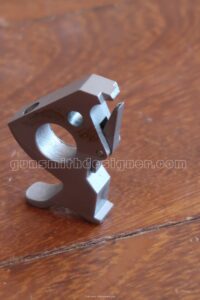
The hammer is a massive, wide, and well-finished component. A hole is drilled clean through it to reduce weight, which also increases lock time and hammer speed. The single-action sear notch is crisp and well-defined with a sharp edge.
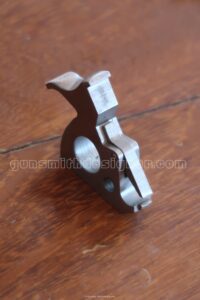
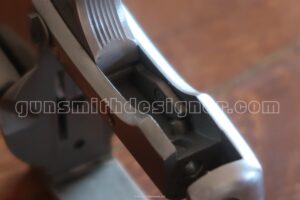
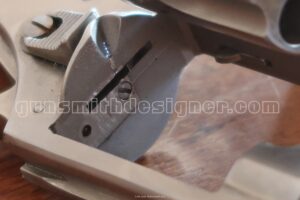
The trigger is also produced via investment casting. The cylinder hand and the transfer bar safety are linked directly to the trigger assembly. These two parts are relatively thin and appear somewhat delicate. The trigger also actuates the cylinder stop, which can be seen inside its frame slot in the photos.
The hammer pivot is a small screw with very few threads. It strikes me as somewhat undersized for this role.
The mainspring is a traditional coil spring. Although it feels smooth, its force combines with the mass of the hammer to ensure positive, reliable primer ignition.
The action is pleasant to cycle in both single and double action, with no discernible hard points or grittiness.
The Cylinder
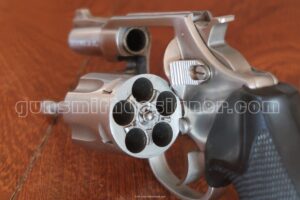
I won’t dwell too much on the cylinder, as its design is quite conventional. The component is well-finished and does not appear to be investment cast—or at least, it bears no manufacturing marks suggesting so.
It would be interesting to know if the company produces its cylinders in-house or outsources them. Manufacturing a cylinder requires a significant number of precise machining operations. Outsourcing this task can be more cost-effective if a reliable, long-term supplier is located nearby.
The cylinder assembly is not easy to detail-strip completely. The main difficulty lies in removing a small pin located inside the central crane axis—an operation that would be much easier if one had three hands.
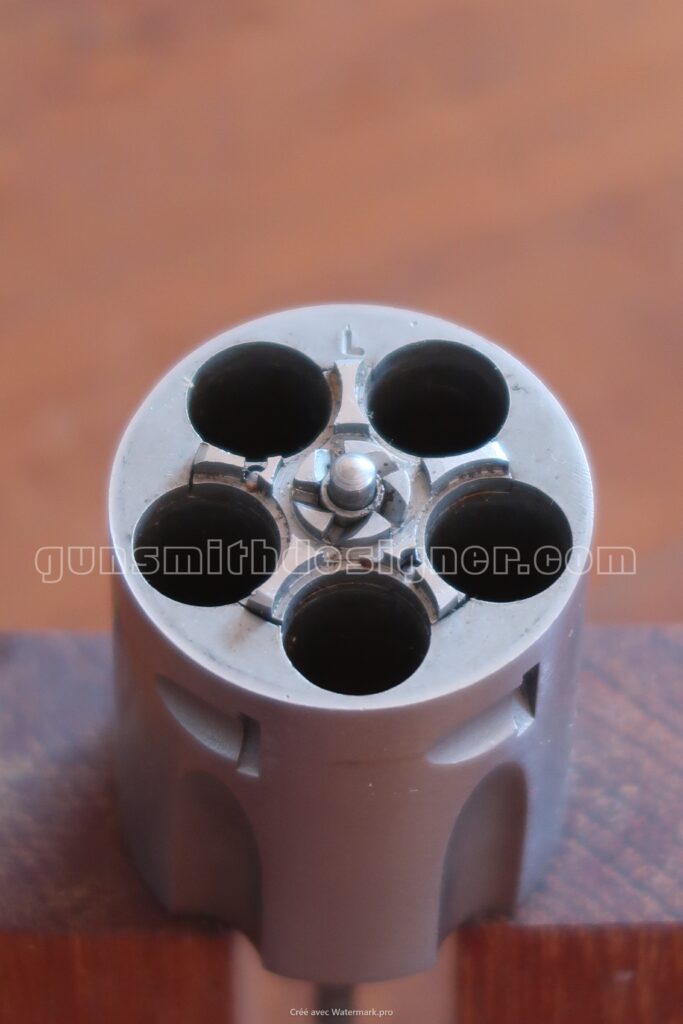
The letter “L” is stamped on the rear face of the cylinder. The same letter is also stamped underneath the barrel.
The cylinder measures 38.5 mm in length and 33 mm in diameter.
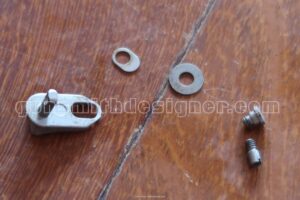
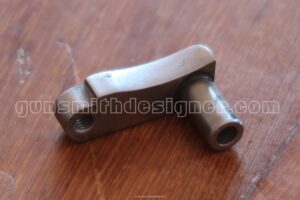
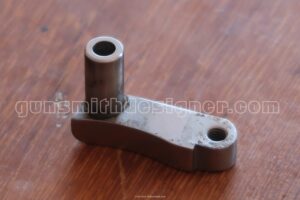
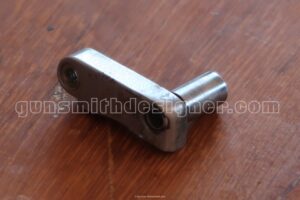
The cylinder crane (pivot) is made via investment casting and appears to consist of two separate pieces. How these two parts are permanently joined—whether threaded, press-fit, or glued—remains unclear, as does the long-term durability of this assembly. A dedicated stress test or warranty repair data would provide a clearer answer. On higher-end revolver brands, this specific component is typically much more complex.
The Barrel
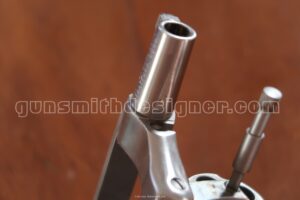
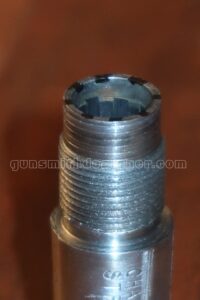
The barrel measures 47.7 mm and features 8 left-hand twist grooves. Its external profile is tapered.
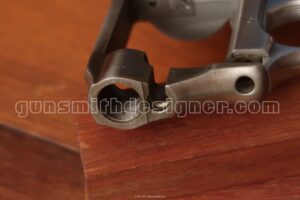
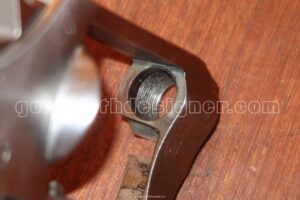
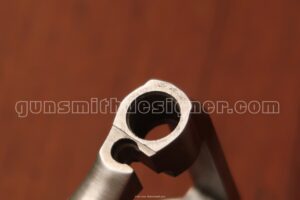
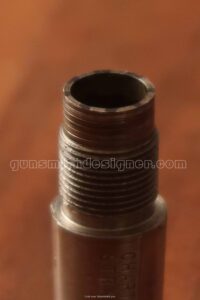
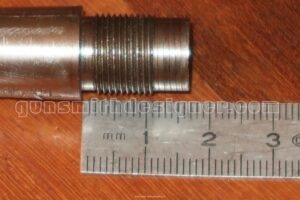
It is threaded tightly into the frame. The thread pitch is 12.7 mm x 28 threads per inch (TPI).
I found no evidence of thread-locking compounds; the barrel appears to be secured purely by torque. Due to a lack of time to fabricate specialized armorers’ tools, I was unable to measure the exact torque value used.
The Sights
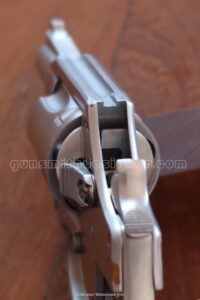
As fits a dedicated defensive firearm, the sights are fixed. The rear sight consists of a simple notch machined directly into the top strap of the frame.
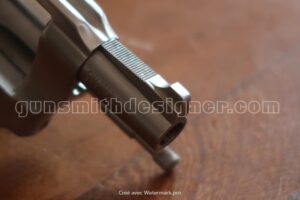
The front sight is pinned or integrated onto the tapered barrel. On post-1985 versions, the barrel assembly becomes more complex as it incorporates a full shroud to protect the ejector rod.
Marketing
In a highly competitive market, a robust customer support policy can be essential to retaining consumers. Charter Arms revolvers come with a lifetime warranty, reflecting the company’s core philosophy.
Conclusion
I deliberately chose to connect this article to the past by anchoring it in the early historical origins of the revolver. Doing so reminds us that a common thread exists throughout small arms history—one shaped by technological breakthroughs, available resources, manufacturing choices, and consumer preferences. Even in the modern era of CNC machining, where numerous operations still require manual labor, manufacturers constantly strive to streamline production. This highlights the value of looking back to identify these recurring engineering patterns.
Since the advent of highly reliable, compact, and high-capacity semi-automatic pistols, one might wonder why manufacturers continue to design and build wheelguns today. Whether driven by personal preference or because they are deeply embedded in the collective cultural consciousness, revolvers have proven themselves through countless historic and rugged environments. If they survived through turbulent times, it is because they possessed the mechanical reliability required, and perhaps because no other suitable tools were available at the time. See articles available here :
The Charter Arms firm is relatively obscure in France. Like any other manufacturer, it must sell to survive, forcing it to market its firearms in a highly competitive American landscape. Countless criteria compete when a consumer chooses a compact defensive weapon, with retail price being one of the most critical. To hit a low price point, a manufacturer must decrease the labor hours spent on each firearm, optimize production tooling, minimize component costs, reduce part counts, streamline staff, outsource specific tasks, and develop an accessory line to offset low margins on the base firearm.
The Undercover mechanism is a textbook example of this approach. It utilizes rapid manufacturing processes that are, nonetheless, highly mastered. Is that a flaw?
The Undercover is not without its merits. Despite this specific specimen being an older production model, it has withstood the test of time remarkably well—a testament, in my opinion, to its sound design and solid execution. Within its price class, the Undercover is quite well-finished. It remains to be seen how these multiple manufacturing simplifications hold up over thousands of rounds, though various online videos can help owners diagnose any common issues that might arise after purchase.
Although I did not find answers to all my technical questions, I would like to thank Ms. Ashley Eckert from Charter Arms, who graciously answered several of them. Obtaining proprietary technical data is always challenging, as industrial property rights often clash with public dissemination. Sharing this technical small arms knowledge is the exact reason why Gunsmithdesigner.com was created.