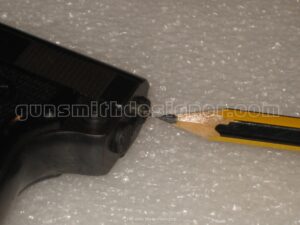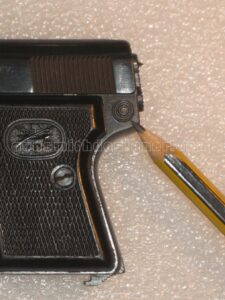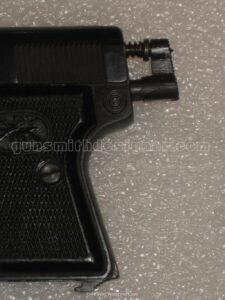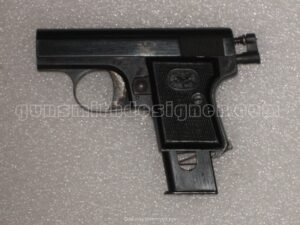
The Bernardelli baby pistol in 25 acp 2/2

This second article on the Bernardelli baby pistol is the sequel to the first, published a few weeks ago. The following chapters will deal with the carcass, the description of the successive stages of a shot start, the loader, the shot with the Baby pistol and the conclusion. Good reading …

The frame

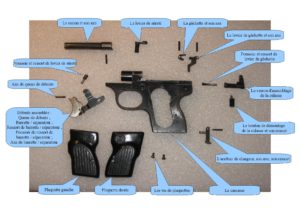
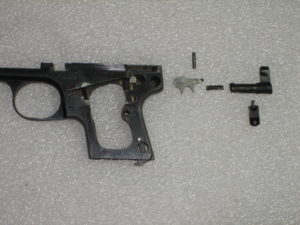
The frame subassembly is composed of 23 parts:

  • The frame ;
  • The left grip ;
  • The right grip ;
  • The screw’s grip ;
  • The lever savety’s spring ;
  • The lever savety ;
  • The trigger bar ;
  • The trigger ;
  • The sear ;
  • The pin’s sear ;
  • The magazine safety ;
  • The pin’s magazine safety ;
  • The lever assembly ;
  • The spring and push of lever assembly ;
  • The slide bolt catch ;
  • The slide bolt catch’s spring ;
  • The pin of the magazne catch ;
  • The magazine catch ;
  • The return lever of the trigger tail ;
  • The magazine catch’s spring.

Gunsmith disassembly of the carcass

The dismounting “gunsmith” of the carcass is pleasant to do because several operations do not require tools. The only useful tools are a screwdriver and a pin punch 1.5 to 2 mm in diameter. Here are the steps:

      • Remove the separator ;
      • Using a screwdriver, remove the right and left stick pads (be careful not to lose the safety lever spring in the left pad) ;
      • Remove the safety lever ;
      • Remove the trigger bar ;
      • Remove the trigger ;
      • Using a pin punch with a diameter of 1.5 to 2 mm, extract the trigger pin.
        You can then disassemble: the trigger, the assembly lever, the assembly lever spring and push, the assembly lever lock, the assembly lever lock spring ;
      Bernardelli Baby 6,35 mm / 25 acp

      • Using the same-hunting pin, extract the loader safety pin and disassemble the loader safety ;
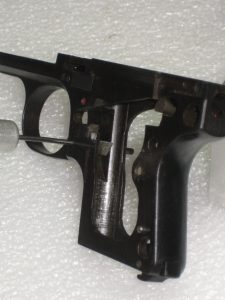
    • The last action is to come to hunt, always with the same punch-pin, the charger lock pin.
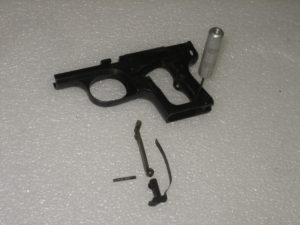
    At the end of these steps, the weapon is completely dismantled.

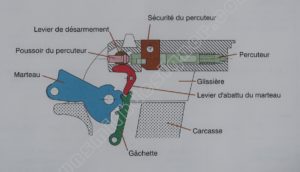
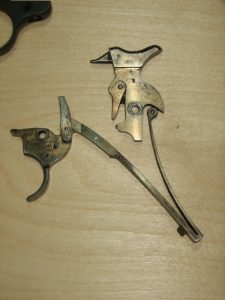
    The trigger and sear mechanism

    The mechanism has few parts. Although small in size, they are well machined and adjusted.

    Some machining of the carcass are complex including the housing of the trigger. The thickness of the walls of the feeder well are fine (1.2 and 1.36 mm). And yet the pieces are terribly well finished.

    The operation of the magazine safety: the latter pivots around an axis and is driven by a small spring. When the loader is not present, the loader safety tilts under the action of its spring and prevents the movement of the trigger tail. In the event that the spring of the magazine safety is broken and / or it is difficult to find one, it can be considered to temporarily remove the loader safety of the weapon (disassembly is explained in the previous chapter) in order to continue using it the time to get the missing items. The removal of this piece does not prevent the weapon from functioning. However, we must not forget that a security has been removed and so that it can change your habits.

    What happens when the shooter presses the trigger, (take the case where a magazine is engaged, the striker is armed, the breech is closed, a munition is chambered):

    1. The shooter presses the trigger. By pressing the trigger, the shooter moves the bar back. The two pieces are connected to each other;
    2. The bar being in contact with the return lever of the trigger tail, it pivots about its axis. The return lever of the trigger tail is moved by the force of the common spring loader lock;
    3. Moving the trigger lever of the trigger tail back releases the trigger. Indeed, this part is a lock for the trigger, it prevents it from going down and thus release the striker in various circumstances.In other words: after a certain stroke of trigger, the trigger is no longer locked;
    4. The shooter continues his action on the tail of relaxation.The back of the bar comes into contact with the trigger and forces it to turn (down) about its axis;
    5. After some relaxation tail stroke, the striker is released;
    6. The striker spring relaxes;
    7. Under the action of the striker spring, the striker is launched on the primer of the cartridge;
    8. The primer is struck, the flame produced ignites the powder;
    9. Under the action of the gases produced by the powder of the cartridge, the walls of the case expands and sticks against the walls of the chamber, there is sealing;
    10. The ammo leaves its location in the cartridge case.The warhead comes out of the barrel;
    11. The impulse produced by the expansion of the gases is channeled through the barrel. It acts on one side on the projectile and on the other side on the case of the cartridge and the breech;
    12. Once the warhead comes out of the barrel, the internal pressure drops. The case retracts, it no longer sticks to the room;
    13. The energy gained by the breech breaks the inertia of the breech. The breech begins to retreat;
    14. About 7 mm after the start of opening, the separator lowers and disengages the trigger from the grip of the bar;
    15. The released trigger returns to its high position under the action of its spring;
    16. Ejection of the drawn socket;
    17. Pushed by the lifting board and the magazine spring, the next ammunition of the magazine takes its place on the lips of the magazine;
    18. The armor of the firing pin protrudes beyond the arm’s length of the trigger, when the firing pin is armed;
    19. The recoil of the breech is damped by the recuperating spring;
    20. The recuperating spring decompresses, the breech begins its race forward;
    21. A new ammunition is pushed towards the room;
    22. The striker is held back by the trigger;
    23. At the end of the cylinder head closure, the separator resumes its place under the action of the return lever of the trigger tail;
    24. Returning forward the return lever of the detent tail causes the bar to go up and thus back to the contact of the trigger;
    25. The shooter releases the pressure on the trigger tail;
    26. The bar resumes its place;
    27. The weapon is ready to repeat the same cycle if the shooter presses the trigger tail again.

    The magazineThis subset is composed of 05 pieces:

    • The magazine body;
    • The lifting board spring;
    • The lifting board;
    • The magazine bottom lock;
    • The charger bottom.

    The magazine is a sheet that has been stamped and welded. It is surprising to see that the weld is not located at the back but on the left side. This is unusual especially since the Baby gun magazine has side openings. The piece is perfectly made and has not suffered from past uses. The welding is fine and not very visible, it shows no sign of weakness. The location of the side openings is clearly not a problem for the weld.

    There are two types of magazine for this weapon. A version in 5 moves and one in 8 moves. The latest version protrudes from the weapon and acts as a handle extension. The addition brings greater comfort to the user but gives a little more volume to the weapon. We can not have everything.

    Few people completely and regularly dismantle the magazine of their weapon. It is a mistake because this cleaning allows to remove any kind of deposit, such as: dust pile, stuffed animals, firing residues, oil … which can at some point block the lifting board and make it inoperative. food. What’s more useless than a defensive gun that does not work when you need it. If you do not do the disassembling and cleaning yourself, have a conscientious connoisseur do it better to see a professional.

    You will find below the operating mode for the disassembly of the charger:

    • Using a tool, push the magazine bottom lock into the interior;
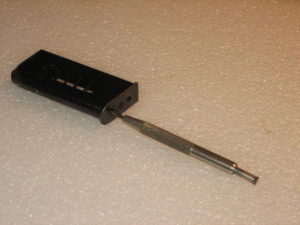
    Insérer un outil

    • Push the feeder bottom towards the front of the feeder;
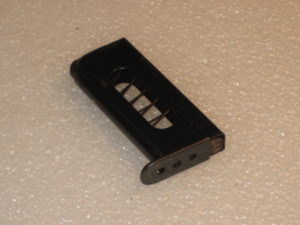
    Le fond de chargeur est déverrouillé.

    • Remove the loader bottom completely, taking care to hold the loader bottom lock and the spring of the lifting board;
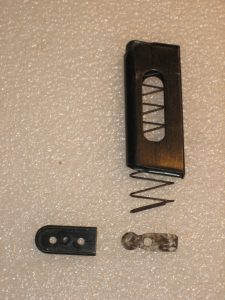
    Le fond de chargeur et son verrou son déverrouillé.

    • Remove the lifting board and its spring;

    Pay attention to the disassembly direction so as not to make mistakes during reassembly.

    On the model at my disposal, the lifting board has side flanges that improve the guidance. The part seems to be executed by stamping a flat sheet.

    The shot Bernardelli Baby

    Shooting with this small weapon is very nice. The recoil is small, equivalent to shooting a 22 Lr ammunition in a similar weapon. The accuracy has not been tested for lack of available ammunition and the weapon is not really intended for marksmanship.

    The average pressure of a 6.35 mm cartridge is 1300 bar (source: CIP standard). The test pressure: 1690 bar (source: CIP standard). For a ball weight of: 3.2 grams, a speed of: 200 meters per second this gives us a warhead energy of: 70 joules (Fiocchi catalog).

    The power of stopping the 6.35 mm is not enough to stop the attacks of a decided individual. Even less if he is under the influence of narcotics or in a state of delirium. The interest of the weapon is its very small volume but not its stopping power. In some ways, it can be reassuring to have this type of defense weapon in your pocket (if the regulations allow you) but it must be borne in mind that it will not necessarily be enough to get you out of bad situations. 

    Conclusion

    It should not be easy to machine small parts in series. V.Bernardelli’s Baby pistol is nevertheless very well done. No traces of machining are visible. Industrial choices are bold but mastered. The aesthetics is very nice. The weapon is well proportioned and well balanced.

    It would be very interesting to compare the weight of the cylinder heads, the strength of the recovery spring of the versions in 22 short and 6.35 mm to relate these data with the average pressure and the ball weight of the two calibers mentioned. This would make it possible to determine a typical breech weight, a standard barrel length, a typical spring recovery force for a given caliber and then compare them again with data from other manufacturers. If you have this information, they interest me.

    The realization of a “torture test” and the analysis of the results provide a lot of information on the design and life of a weapon. While the latter is not intended for intensive shooting, what would be the behavior of the Baby gun during a torture test? After how much ammunition fired would the first piece break? What would be the first cased pieces? Are the same pieces breaking at the same time? How to cure it ? To this day, I do not know if the firm Bernardelli performed this kind of test for this weapon. It would be interesting to have access to the results of one of these tests.

    The choices of the designers, the validators of these choices are of great importance. Good technical choices will allow the weapon to become an icon of its category and to go through the years to become a timeless object. The design, the realization, the promotion, the marketing are deeply linked stages which, if they are successful, will anchor a weapon in the thoughts. We will find this weapon many years after its manufacture always in working order (because well designed), always pleasant to look at or use. Time will give it a charming patina and a greater value. I think the Baby gun is one of them.

Posted in All articles, Handguns | Leave a comment

The Bernardelli baby pistol in 25 acp 1/2

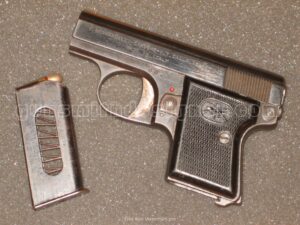
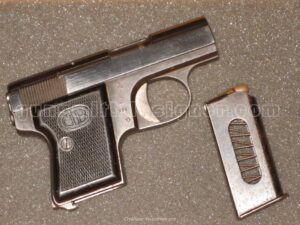
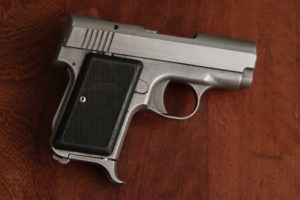
Today, I have the opportunity to write about the V. Bernardelli Model 68, also known as the “Baby.” The firearm I am presenting to you is chambered in 6.35mm or .25 ACP.

I wanted to talk about this handgun because I did not expect to find such a beautiful finish on an arm of this type—namely, a small pocket defense pistol. The second reason for writing this article is how the barrel mounts to the frame. It is quite unusual, extremely well executed, and well worth taking a closer look at.

Bernardelli Baby Specifications

I will not go over the history of this handgun, as I do not have much data on the matter. It seems that the first models appeared in the 1940s/1950s. You can find the history of the V. Bernardelli company by clicking on the brand’s logo.

Logo V.Bernardelli.

A version of this firearm exists in .22 Short. It would have been useful to compare both models to highlight their common points and differences. However, I was unable to gather both versions at the same time. Therefore, I cannot make that comparison today. Hopefully, the future will grant me the opportunity to conduct this experiment later on.

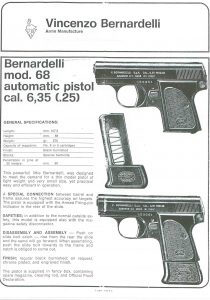
Bernardelli Baby 6,35 mm manuel

  • Overall Length : 106.5 mm ;
  • Overall height of the weapon : 69 mm (with the 5-rounds magazine), 68.5 mm (without magazine) ;
  • Width : 20.5 mm ;
  • Weight : 260 grams (with an empty 5 rounds magazine) ;
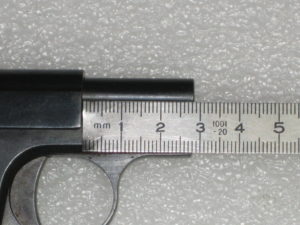
  • Barrel length : 53 mm ;
  • Caliber : 6, 35 mm Browning or 25 acp ;
    • Capacity : 5 to 8 depending on the magazine (a 5 round magazine is featured here) ;
  • Mechanism type : single action ;
  • Safety lever : Located on the left side of the frame ;
  • Magazine safety : yes ;
  • Grip : good handling, despite the small volume of the firearm ;
  • Material : entirely made of steel (except the grip panels) ;
  • Number of parts : 39.

Field Stripping the Bernardelli Baby :

Field stripping this firearm does not require any special tools. The various steps to complete this task are detailed below :

  • Handling any firearm can cause serious damage. Consequently: always point the firearm in a safe direction away from yourself or others, ensure the weapon is unloaded (no magazine engaged), and check that the chamber is empty ;
  • Remove the magazine from the firearm ;
  • Verify that the chamber is empty ;
  • While checking the chamber, you will likely cock the striker (depending on how far back you pull the slide). It takes a 23mm rearward slide stroke to cock the striker. You can tell the striker is cocked when a small pointed piece protrudes from the back of the slide ;
  • Press the button located on the rear of the frame, on the left side of the firearm ;
  • Regardless of the striker’s position (cocked or uncocked), the assembly lever will pop out of its housing under the pressure of the striker spring and the sear spring ;
  • Push the striker spring back inside the slide. To do this, if the striker was cocked during previous manipulations, you must engage an empty magazine (just enough to disengage the magazine safety from the trigger bar, see the next photo) and pull the trigger (hence the importance of having checked that the chamber is empty);
  • Remove the magazine again ;
  • Pull the slide back a few millimeters to disengage the extractor from its slot ;
  • Once the extractor is disengaged, lift the rear of the slide ;
  • When lifting the rear of the slide, be careful not to lose the disconnector. It is prone to slipping out. We will look at the role of this part later on ;


  • Under the action of the recoil spring, the slide will slide off its housing toward the front. Guide the slide through this movement. Be careful not to lose the disconnector, the striker spring, the striker, the recoil spring, and its guide rod ;
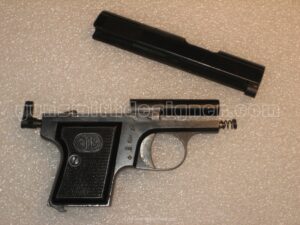
  • To remove the barrel, extract it by pushing it to the left (on my specific model, it comes out through the left side) ;
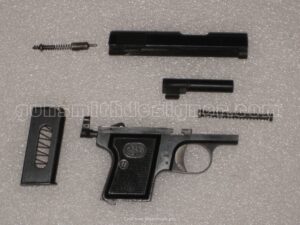
  • Field stripping is now complete; you are left with the following components ;

The Bernardelli Baby Sub-assemblies

The sub-assemblies of the 6.35mm Bernardelli Baby pistol are :

  • The slide / barrel sub-assembly ;
  • The frame sub-assembly ;
  • The magazine sub-assembly.

The Slide / Barrel Sub-assembly

The slide/barrel sub-assembly of the studied weapon consists of 11 pieces:

  • The slide ;
  • The extractor ;
  • The extractor spring ;
  • The extractor pin ;
  • The barrel ;
  • The recoil spring ;
  • The guide rod ;
  • The striker ;
  • The striker spring ;
  • The striker spring guide/cocking indicator ;
  • The cocking indicator return spring.

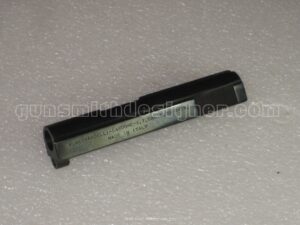
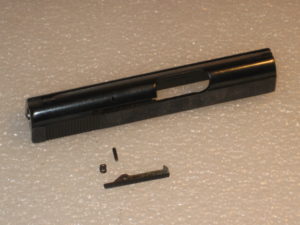
The slide is made of steel. Its dimensions fit within a volume of: 15.4 mm (width) x 21.5 mm (height) x 104 mm (length).

The weight of the part (with the extractor) is 72 grams. The distance between the underside of the slide (or top of the frame) and the barrel axis is 4.5 mm.

The breech face diameter (where the cartridge casing base sits in the slide) is 8 mm with a depth of 0.94 mm.


The maximum travel of the barrel inside the slide (the same with or without the recoil spring) is 28 mm, while a live round measures approximately 22.8 mm.

Bernardelli Baby

Advanced disassembly of the slide components involves driving the extractor pin out of its hole using a 1.5mm pin punch. The pin is thin and short. The extractor spring measures 3 mm in length with a diameter slightly under 3 mm. These parts are very small: be careful not to lose them. Stripping these parts gives you proper access to clean the extractor slot. This area is rarely accessible, making it the perfect opportunity to do a thorough job. Clean the parts before reassembly as well.

Vue de l'extracteur démonté

The striker body diameter is 5.96 mm. The striker tip diameter is 2 mm. The overall length of the striker is 19.5 mm. It would be interesting to compare the striker of this 6.35mm version with that of the .22 Short version. Indeed, firing a rimfire cartridge like the .22 Short requires striking the rim of the casing. In this case, two layout options seem possible:

  • Either increase the striker body diameter to 7 mm (the rim diameter of a .22 Short rimfire round) and then offset the striker tip to the periphery of the 7mm cylinder ;
  • Or offset the striker channel itself ;
  • Or apply both solutions simultaneously.

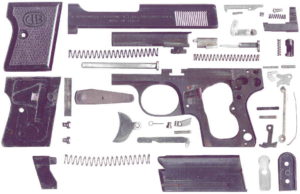
Which option did the manufacturer choose? To this day, I do not have the exact answer because I do not have access to the dimensions of the .22 Short part. However, a schematic of the .22 Short version helps our analysis. On the exploded view below, we can see the shape of the striker, but also that ejection is not operated by the striker itself, but rather by an extension of the striker spring guide rod.

Vue éclaté du pistolet Bernardelli Baby en calibre 22 short. On remarquera la forme de l'éjecteur et du percuteur.

The slide does not move along the frame via machined rails like on most automatic pistols. The slide is guided at two specific points :

  • The first guide point is the barrel, as the front of the slide cycles around it ;
  • The second is the assembly lever. By entering the striker channel, it restricts the slide’s path.

    After firing, the slide requires a rearward travel of 23 mm for the striker to cock again. The striker’s cocking lug does not protrude from the bottom of the slide. It is the sear that catches it as it cycles. The striker also functions as the ejector. At the end of the slide’s rearward travel, the tip of the striker protrudes by 3.6 mm through the breech face, giving an impulse to the empty casing, which pivots around the extractor and ejects.

The barrel fits within a volume of: 53 mm (length) x 11.7 mm (width) x 14.4 mm (height). The outer diameter of the round section is 9.8 mm. The weight of the barrel is 21 grams. The rim of the cartridge remains outside the chamber.

Was the barrel rifled after its profile was machined? Or did the rifling happen first, followed by the profile machining? This would be interesting to know. I would lean toward the second option (as it is the most common). Namely: using steel bars several tens of centimeters long, drilled and rifled to the 6.35mm caliber. The bars are then cut to the desired length. The barrel’s outer profile is obtained by machining these cut portions. Finally, the chamber is cut using a specific chamber reamer. The Bernardelli Baby barrel can be manufactured from a rifled blank of 14 mm minimum diameter. The barrel features 6 left-hand grooves.

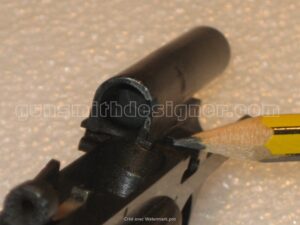
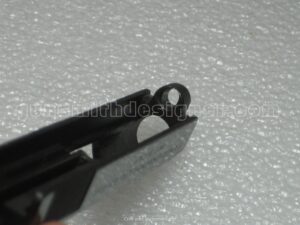
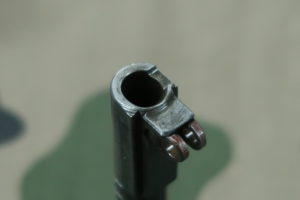
One of the significant design choices on this handgun is the mounting method chosen by V. Bernardelli to lock the barrel to the frame. This type of mounting is rarely utilized. The barrel is secured to the frame via an inverted T-shaped interlocking fit. The barrel slides laterally into a matching groove machined into the frame. The machining does not feature simple rectangular shapes (which one might expect) but rounded curves. While machining the female housing requires a specific form cutter, the male lug requires more complex machining and fitting. I believe this choice reflects the manufacturer’s desire to prevent stress cracks from developing in the corners (particularly the upper corners) which a sharp rectangular shape would be prone to. The fit on my specific handgun is exceptionally well crafted; once seated on the frame, the barrel exhibits almost no play.

The width of the T-lug base is 11 mm. The height of the T-lug base is 2 mm.

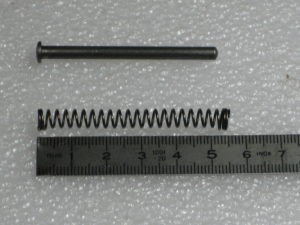
The recoil spring has a length of 55 mm. The wire diameter is 0.7 mm. The spring flares out at both ends. At its center, the outer diameter is 5.7 mm. The flared ends have an outer diameter of 6.6 mm.

The guide rod has a length of 53.6 mm with a body diameter of 4 mm.

Bernardelli Baby, vue de la tige guide et du ressort récupérateur.

To be continued in a future article.

Posted in All articles, Handguns | 11 Comments

The rifle mle 1866 Chassepot 2/2

Through the transcription of an article tinged with a hint of optimism published in 1869, we saw the early adoption of the new standard-issue French rifle: the Chassepot Model 1866.

A weapon firing so many cartridges that the enemy would be quickly torn to pieces in the event of a conflict,’ according to the pre-war article (referring to the war of 1870).

The first article is available here : The rifle mle 1866 Chassepot 1/2

What is the situation in 1873 ? What can be deduced throught the study of more recent texts ? Is there à connection with more contemporary events ?

The adoption of the Chassepot Mle 1866 rifle

In 1865, while the permanent commission of Versailles had chosen a muzzle-loading rifle to replace the standart-issue rifle, Emperor Napoleon III expressed the wish to adopt a breech-loading rifle. Indeed, Prussia’s recent victories forced a more modern choice. This state had adopted a breech-loading rifle decades earlier (1840) : the Dreyse rifle. 

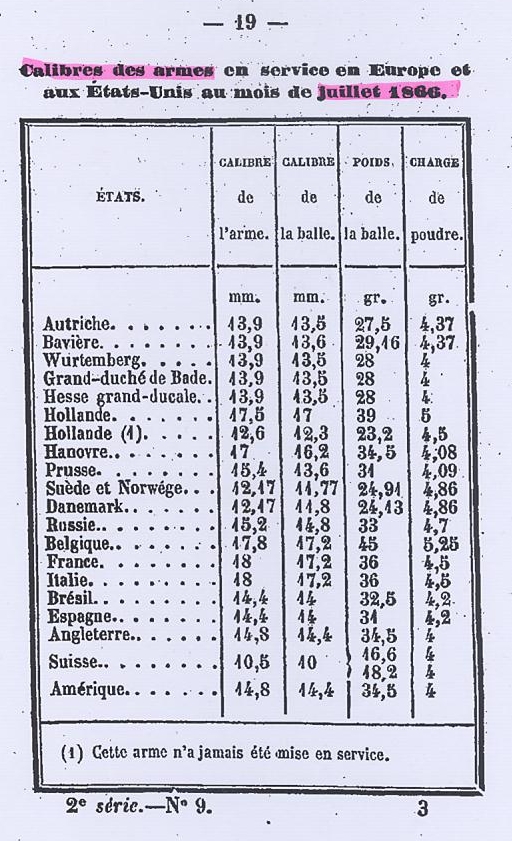
Under Swiss influence, the trend of the area learned toward a reduction in caliber. The goal was a weapon with a coliber between 10 and 15 mm in order to achieve a flatter trajectory and allow firing at greater distances, which was less feasible with a 17 or 18 mm projctile. The aim was thus to heavily impact, or even defeat, the ennemy before hand-to-hand combat.

Table of load differences (diameters, bullet weights, powder charges).

It is a period of rapid technical developments, and many directions exist. However, selection tests are carried out using a rifle that is retrograde but still deeply rooted in people’s minds: the percussion rifle. The latter ultimately represents a benchmark of old weaponry and an old way of waging war. On the other hand, no metallic cartridge weapon is present in the ranks; it is too early for France.

Ultimately, the commission is tasked with ruling on three weapons: the Chassepot rifle, the Chassepot rifle modified by Mr. Plumerel, and a muzzle-loading rifle. The Chassepot rifle was adopted.

The creator of the Mle 1866 rifle is the author of three patents: the rubber obturator, the bolt action mechanism derived from the Prussian Dreyse, and the cartridge. The ballistic characteristics of the barrel and the bullet (bullet length/caliber, bullet weight/powder charge, shape and pitch of the rifling/influence of the projectile’s rotation) were defined based on studies by various contributors and commissions, and then applied to the Chassepot mechanism.

On February 14, 1866, an order for 1,500 weapons was placed with the Châtellerault manufacture.

In June 1866, 400 rifles were received. They would be sent to the Châlons camp to be tested by the Imperial Guard (see the first article on the Chassepot rifle).

On July 3, 1866, the manufactures of St. Étienne and Puteaux were created. The objective was the manufacturing of 150,000 weapons per year and 1,800 machine tools intended for the factories

The Mle 1866 rifle is a resolutely modern weapon for its time. Terribly well-made, it demanded a significant effort from the nation. Then comes the time for the first trials, followed by the trial by fire. The single criterion of the individual firearm is not enough to predict the victor of upcoming battles.

Has the idyllic framework described by the first article evolved? What about the best weapon in Europe? Are Mr. Chassepot’s patents adapted to a weapon of war quickly built before a major conflict? Or to a target rifle? Will the time between the delivery of the rifles and the start of the war be sufficient to remedy the various technical problems ?

The Weapon’s Defects

Gas blowback toward the shooter’s face (synonymous with a lack of gas seal) was the reason for the delayed adoption and proliferation of breech-loading weapons. Mr. Chassepot used a material that was recent for the era—a rubber washer—to achieve this seal, which, as a side benefit, reduced the weapon’s recoil. The part deteriorated in various ways: it cracked, melted and blocked the needle channel, or lost its elasticity. The blowback increased progressively as the washer lost its diameter while melting. The soldier carried a replacement part in his cartridge pouch. The use of this material was a bold choice; to this day, very few firearms have used rubber for this function, and the Chassepot may be the only one.

As seen above, the seal was more or less effective toward the outside. The same applied to the inside. Gases resulting from powder combustion travel anywhere they encounter no resistance. Consequently, they blew back into the bolt through the firing pin needle channel. This resulted in annealing (softening) the striker spring, leading to weak strikes or even spring breakage. In some cases, it was possible to cock the hammer (the striker) by slamming the buttplate on the ground. Combustion gases also heavily fouled the inside of the bolt.

Fouling did not only affect the inside of the bolt, but the chamber as well. Debris and shooting residue remained inside, preventing the chambering of subsequent rounds. 

The needle’s diameter was 1.5 mm. Doubling the diameter to 3 mm would provide four times the strength, according to a study from that era.

Forcefully closing the bolt could cause an accidental discharge of a cartridge. This slamming action occurred due to the absence of a locking cam/inclined closing ramp on the receiver. The presence of this machining helps the shooter progressively push the ammunition into the chamber while locking the bolt. The vast majority of modern bolt-action weapons feature this ramp, providing unparalleled smoothness.

The weapon’s polished white finish, besides being highly visible from afar, required significant maintenance to prevent corrosion.

Despite the speech by Mr. Thiers, President of the Republic, on June 8, 1872 :

“In the opinion of military men, the Chassepot rifle was the best weapon in use among armies. The Chassepot rifle is recognized as excellent, except for its cartridge, which every European country is seeking to improve…”

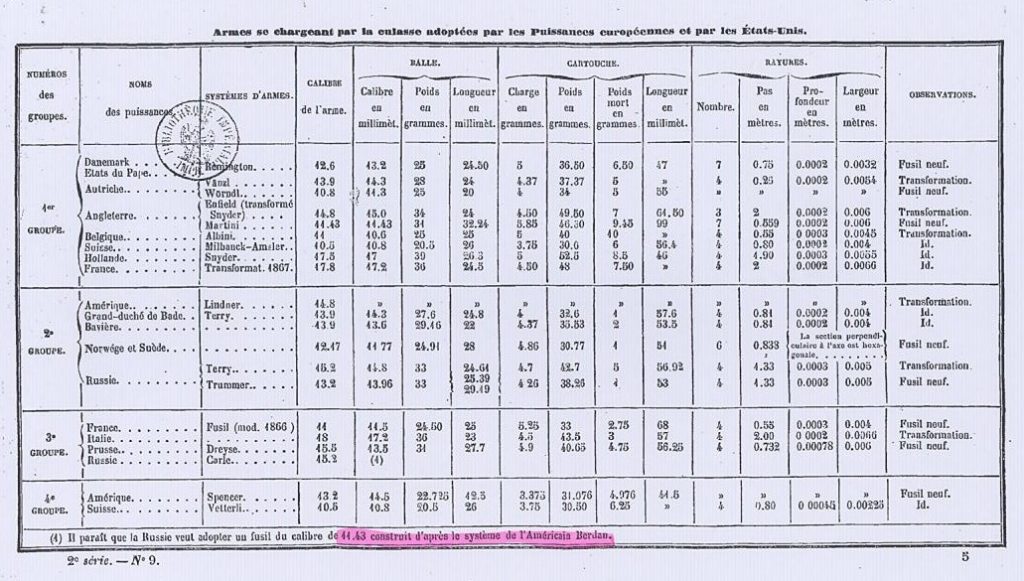
While it is necessary to keep in mind the industrial context of the era, as well as the speed with which the weapon was manufactured and distributed, it still seems that several criticisms can be leveled against the Chassepot rifle’s design, contrary to the previous article.

Table of breech-loading firearms adopted by European countries and the United States.

The Chassepot Rifle Cartridge

As previously stated, three principles competed during this period of small arms history: muzzle-loading, paper (combustible) cartridge, and metallic cartridge. Although proposed by the Versailles commission, muzzle-loading was deemed obsolete, swept away by the consequences of the Battle of Sadowa.

The combustible cartridge thus found itself in competition with the metallic cartridge. Although certain observers of the era preferred the latter, which were said to be of better quality even when sourced from abroad, its drawbacks received a larger platform. The flaws of the metallic cartridge at the time were :

  • The extra weight of the case. The weight of the casing added to that of the bullet reduces the number of cartridges a soldier can carry ;
  • The chemical reaction between the case and the powder, which can lead to the early decomposition of the gunpowder ;
  • Difficult extraction ;
  • Cases that are prone to splitting ;
  • The requirement of an extractor. A delicate and therefore fragile part, not easily replaced by the soldier on the battlefield ;
  • The cartridge cannot be reloaded or manufactured by the soldier ;
  • The tooling required for mass production is deemed too expensive ;
  • Dimensional variations in the cases due to different manufacturers ;
  • The ammunition’s lack of power ;
  • Chambering difficulties if the case is dented or damaged ;
  • The manufacturing cost of the case.

In 1866, no metallic cartridge weapon was in competition with the Chassepot.

n 1873, the choice between modernity (metallic cartridge) and semi-modernity (combustible cartridge) had not yet been made. Public finances and past military principles led some to argue that the paper cartridge remained the future. The choice would finally be settled in 1874. This was probably the time needed to perfect the metallic case and to overcome a certain resistance to change.

The standard-issue Chassepot cartridge

The specifications of the standard-issue cartridge are :

  • Powder charge: 5.25 grams ;
  • Bullet weight: 24.5 grams ;
  • A bullet lenght of 25 mm (should be closer to 33 mm for greater accuracy, 3 times the diameter) ;
  • Bullet diameter : 11 mm.

According to the 1873 manual on cartridges for military weapons, and notably for the Chassepot rifle, the 5 qualities of a military firearm cartridge should be :

  • 1 Cartridge preservation / shelf life ;
  • 2 Consistency, speed, safety, and shooting accuracy ;
  • 3 The structural strength of the cartridge ;
  • 4 Ease of manufacturing ;
  • 5 Cost-effectiveness / low production cost.

1. Cartridge Preservation / Shelf Life

It is somewhat difficult to imagine good, long-term preservation for paper cartridges loaded with black powder. Furthermore, what kind of preservation are we talking about? The storage of components before assembly, the preservation of the manufactured ammunition, preservation during shipping, storage in ammunition bunkers, preservation during operational transport, or storage in the soldiers’ cartridge pouches… Any of these handling steps, if poorly executed, can cause damage. Combustible cartridge ammunition is fragile; it must be protected from harsh weather conditions—which is no easy task in times of war. The Chassepot cartridge is not ideal in this regard.

2. Consistency

This quality stems from the homogeneity of a batch of cartridges. It therefore depends on numerous criteria such as preservation, the consistency of components, and manufacturing quality… which means the parameters to control are significant, especially if part of the production is outsourced to civilian workshops. To this must be added the irregular deposits left by shooting residue and the paper casing in the chamber, which compromise consistency.

3. Promptness

The rate of fire of the Chassepot rifle is a real advantage compared to a muzzle-loading weapon, even more so because it allows reloading while crouching or lying down. This speed is only possible if the firearm’s chamber is not overly fouled, or if the bullet has not separated from the case inside the soldier’s cartridge pouch… among other issues

3a. Safety

It stands to reason that the Chassepot cartridge does not offer full safety guarantees. The reason has already been mentioned above: there can be no safety when firing caseless ammunition if the breech-loading mechanism is not gas-tight.

3b. Shooting Accuracy

Some of the criteria for shooting accuracy include the centering of the bullet on the barrel’s axis, the consistency of the bullet’s velocity, barrel wear and cleanliness, as well as the uniformity of the bullet’s weight and diameter.

Aligning the axis of the bullet with the axis of the barrel when the chamber is subject to fouling can seem complicated. Likewise, even in a chamber free of residue, there is always some play between the forcing cone (throat) and the bullet, causing a misalignment. This play can be reduced (but not eliminated) by using multiple layers of paper around the bullet, which will always result in compression and therefore irregularity.

Depending on the condition of the bolt’s rubber washer, gas leaks can occur, altering internal pressure and consequently the bullet’s velocity. This impacts the projectile’s trajectory flatness and, as a result, shooting accuracy. Firing residue inside the barrel’s rifling will have the same impact.

4. The Structural Strength of the Cartridge

The structural strength of the Chassepot cartridge was highly inadequate for a military round. It is estimated that 20 percent of the ammunition was damaged during the 1870–1871 conflict, sometimes destroyed directly inside the soldiers’ cartridge pouches during troop movements. Historical accounts describe soldiers fleeing the enemy due to a lack of cartridges, caused by supply failures that failed to arrive… even with the use of the railway.

5. Ease of Manufacturing

By adopting the paper-cased cartridge, decision-makers wanted to allow soldiers the possibility of assembling their own ammunition. In the event of capturing an enemy convoy or camp, fighters could then make use of the powder and primer stocks left behind by the adversary.

However, as ammunition became more complex, it was no longer as easy for soldiers to manufacture it themselves in a war that was becoming increasingly mobile. Instead, reliance shifted toward railways to transport supplies. This marked the beginning of “industrial operational support.” On the other hand, it was easy to set up manufacturing workshops with trained workers and simple tooling. It appears that poor-quality ammunition was delivered by civilian workshops during the 1870–1871 conflict. One worker could manufacture 85 cartridges per ten-hour shift.

Following changes in military practices and the increased range of weapons, ammunition consumption skyrocketed. This was likely one of the primary reasons for the supply shortages.

6. Cost-Effectiveness

In 1873, a military law programs 1,200,000 men under the flag. At a rate of 100 cartridges per staff per year, an annual requirement of 120,000,000 cartridges are required under penalty of insufficient instruction. It is easy to imagine that each component needs to be optimized in order to reduce the cost as much as possible and thus reduce the bill. In view of the annual need for cartridges, the smallest savings passed on each munition represents very quickly large sums. The paper case cartridge remains more economical than the metal case cartridge.

Can we truly say, however, that 100 cartridges a year are enough to train a marksman and maintain a soldier’s skills? This highlights the value of encouraging private initiatives, such as establishing civilian shooting ranges, founding hunting societies, teaching children marksmanship in schools, and offering civilians firearms that closely resembled standard-issue weapons so they could practice year-round without impacting state resources. Traces of these initiatives can readily be found in old manufacturer catalogs.

Many of the criteria listed above were not met; yet, the paper cartridge was accepted.

The Callebaut cartridge

“The Chassepot rifle is recognized as excellent, except for its cartridge, which every European country is seeking to improve.” (Speech by the President of the Republic, June 8, 1872)

Driven by a desire to equip the Chassepot rifle with a more suitable ammunition, the Callebaut firm (Paris) proposed a wooden-bodied cartridge. This new round, devoid of a metallic case, was known as a “chased cartridge” (étui chassé). 

This combustible-cased variant enabled faster shooting, delivering 150 rounds compared to only 101 rounds fired with the standard-issue ammunition. It recorded a single misfire out of 1,089 rounds fired. Furthermore, 207 rounds were fired without any incidents related to the rubber sealing system, compared to 85 in the standard-issue rifle. This improvement was due to the use of a rubber membrane sealing the cartridge tube, which expanded in diameter under gas pressure, thereby reducing stress on the bolt’s rubber obturator.

Upon firing, the 13.5 mm diameter wooden tube was forced into the forcing cone (throat), breaking it apart. The pieces of wood exiting the barrel effectively cleaned it. No wood particles remained in the chamber.

The cartridge’s wooden body was more durable than that of the standard-issue round. According to the manufacturer, even if it were half-crushed, the ammunition would still function. If it still functions… it must have been difficult to chamber.

200 cartridges could be manufactured in ten hours, which is 2.35 times more than standard-issue ammunition. Time was not the only thing saved; wasted or defective ammunition was reduced as well.

This cartridge does not appear to have been adopted by the military. The following year, the Gras rifle would put an end to the paper-cased cartridge; the era of the metallic case had arrived.

I have not found any illustration or depiction of this ammunition.

Conclusion

Through these two articles, one can ultimately see the gap between textbook transcriptions and the reality of war—between theory and practice.

Pressed by Prussian victories, notably the one on July 3, 1866, at Sadowa, France hastily decided to equip its army. It chose a weapon that was modern for its time: the Chassepot Mle 1866 rifle. It used this opportunity to establish new state manufactures. The choice made by France was bold. Modern engineers have not clearly resolved, and thus seldom commercialized, this type of firearm. Indeed, the use of combustible casings is bound to encounter issues that remain difficult to solve even today—most notably, chamber fouling and gas sealing. It was ambitious in 1865–1866 to attempt to replace a standard-issue percussion rifle with a weapon combining several technical advancements, hoping to solve major hurdles all at once (the use of a gas-tight breech-loading mechanism, caliber reduction, fouling caused by black powder, fouling from burnt paper residues, changes in infantry rifle doctrine, the adoption and mass production of a new ammunition, and the use of an uncommon material in gunsmithing at the time: rubber, etc.), all while being manufactured by a newly created factory

The St. Étienne arms manufacture would deliver the ordered weapons shortly before the outbreak of the war. However, what about the training of soldiers, officers, medical services, and various supply lines ?

Germany had taken the lead by equipping its army with breech-loading rifles well before other nations (1841, 25 years before France). This early adoption surely had its setbacks, but by outfitting themselves decades before the others, they had the time to overcome various technical hurdles and train their soldiers, armorers, and officers to make them fully proficient in servicing the weapon.

Germany took the lead in endowing its army with breech-loading rifles well before other nations (1841, 25 years before France). This advance certainly had setbacks but by equipping decades before the others, they had time to stop at various technical events and train their soldiers, gunsmiths, officers to make them more fit to fight.

Following the Ems Dispatch, and despite warnings from Adolphe Thiers, France declared war on Germany. The war lasted from July 19, 1870, to January 29, 1871—just over six months. The result of this lack of preparation was the loss of Alsace-Lorraine, a territory that would remain German until the end of World War I, 47 years later

Fundamental issues directly affecting Mr. Chassepot’s patents should have been experimented with earlier. This would have allowed various civil and military maintenance and supply echelons to rectify certain flaws before the conflict. Alternatively, France should not have declared war on Germany until these anomalies were resolved. Starting in 1874, Chassepot rifles would be converted to fire metallic cartridges. It would then bear the name 1866/74 Gras.

By 1873, America, Great Britain, and Belgium had adopted metallic cartridge firearms. France resisted; the reason may stem from the absence or limitation of private industries, which usually bring forth greater innovation and competition in the hope of securing major government contracts. France preferred the opposite: a monopoly of national manufactures. History demonstrated their potential insufficiency during the war of 1870–1871 and for many years thereafter. To read :

The importance of regimental armorers and private enterprises in advancing the small arms world and rapidly modifying standard-issue weapons is well-established. A nation must nurture knowledge and talent. Today, the state of the arms industry in France is such that private industry is dying out, the St. Étienne arms manufacture is closed, and the French army’s next assault rifle will be German…

Useful Sources for this Article :

Posted in All articles, Ammunitions, Military french guns, Rifles | Leave a comment